

Altium Packaging's plant in Memphis, Tennessee, counts every bottle on its ten bottling lines with BeamTracker and reads their first pass yield as the bottles move: how many of the bottles that started down a line made it through each step, and how many were lost where. Maintenance runs on the same counts in Maintain, so a wear part is inspected on the bottle it is due. The numbers run live on TV screens on the shop floor and in the break room, on desktops and on phones, so the team deals with losses as they happen, not weeks later.
The Challenge
Altium Packaging makes plastic bottles and containers for dairy, water, beverage, food, household and specialty chemical brands. In Memphis, its ten bottling lines run anywhere from 20 to 140 bottles a minute, and every bottle passes through several machines on its way down a line.
A count at the end of a line says how many good bottles came off it. It doesn't say how many started, or where the rest were lost. A bottle can be formed at the first step and rejected at the last, and at 140 a minute a small loss at one step adds up to thousands of bottles a shift. Without a count at every step, the plant could see that a line was down on yield but not which machine was costing it.
The rest of the plant ran on the same delay:
- Reports that took days or weeks. By the time the yield numbers arrived, the shift they described was long over.
- Meetings about the past. The team met over old reports and hoped everyone remembered exactly what had happened at that moment.
- Wear measured in bottles, scheduled by the calendar. The Slide Knife on one of the line's steps needs inspecting every 100,000 bottles. A line that ran fast all week reached the count early, and one that ran slow reached it late, so a date-based schedule was always either early or overdue.
- Losses nobody saw coming. A part that missed its inspection or replacement, or an operator unsure of the role they played in the line, cost production before anyone knew it had happened.
The Solution
Altium Packaging put a BeamTracker at every step of its ten bottling lines, set each line up as one cascade in IoTFlows, and ran its maintenance in Maintain, all on the same live counts.
A count at every step
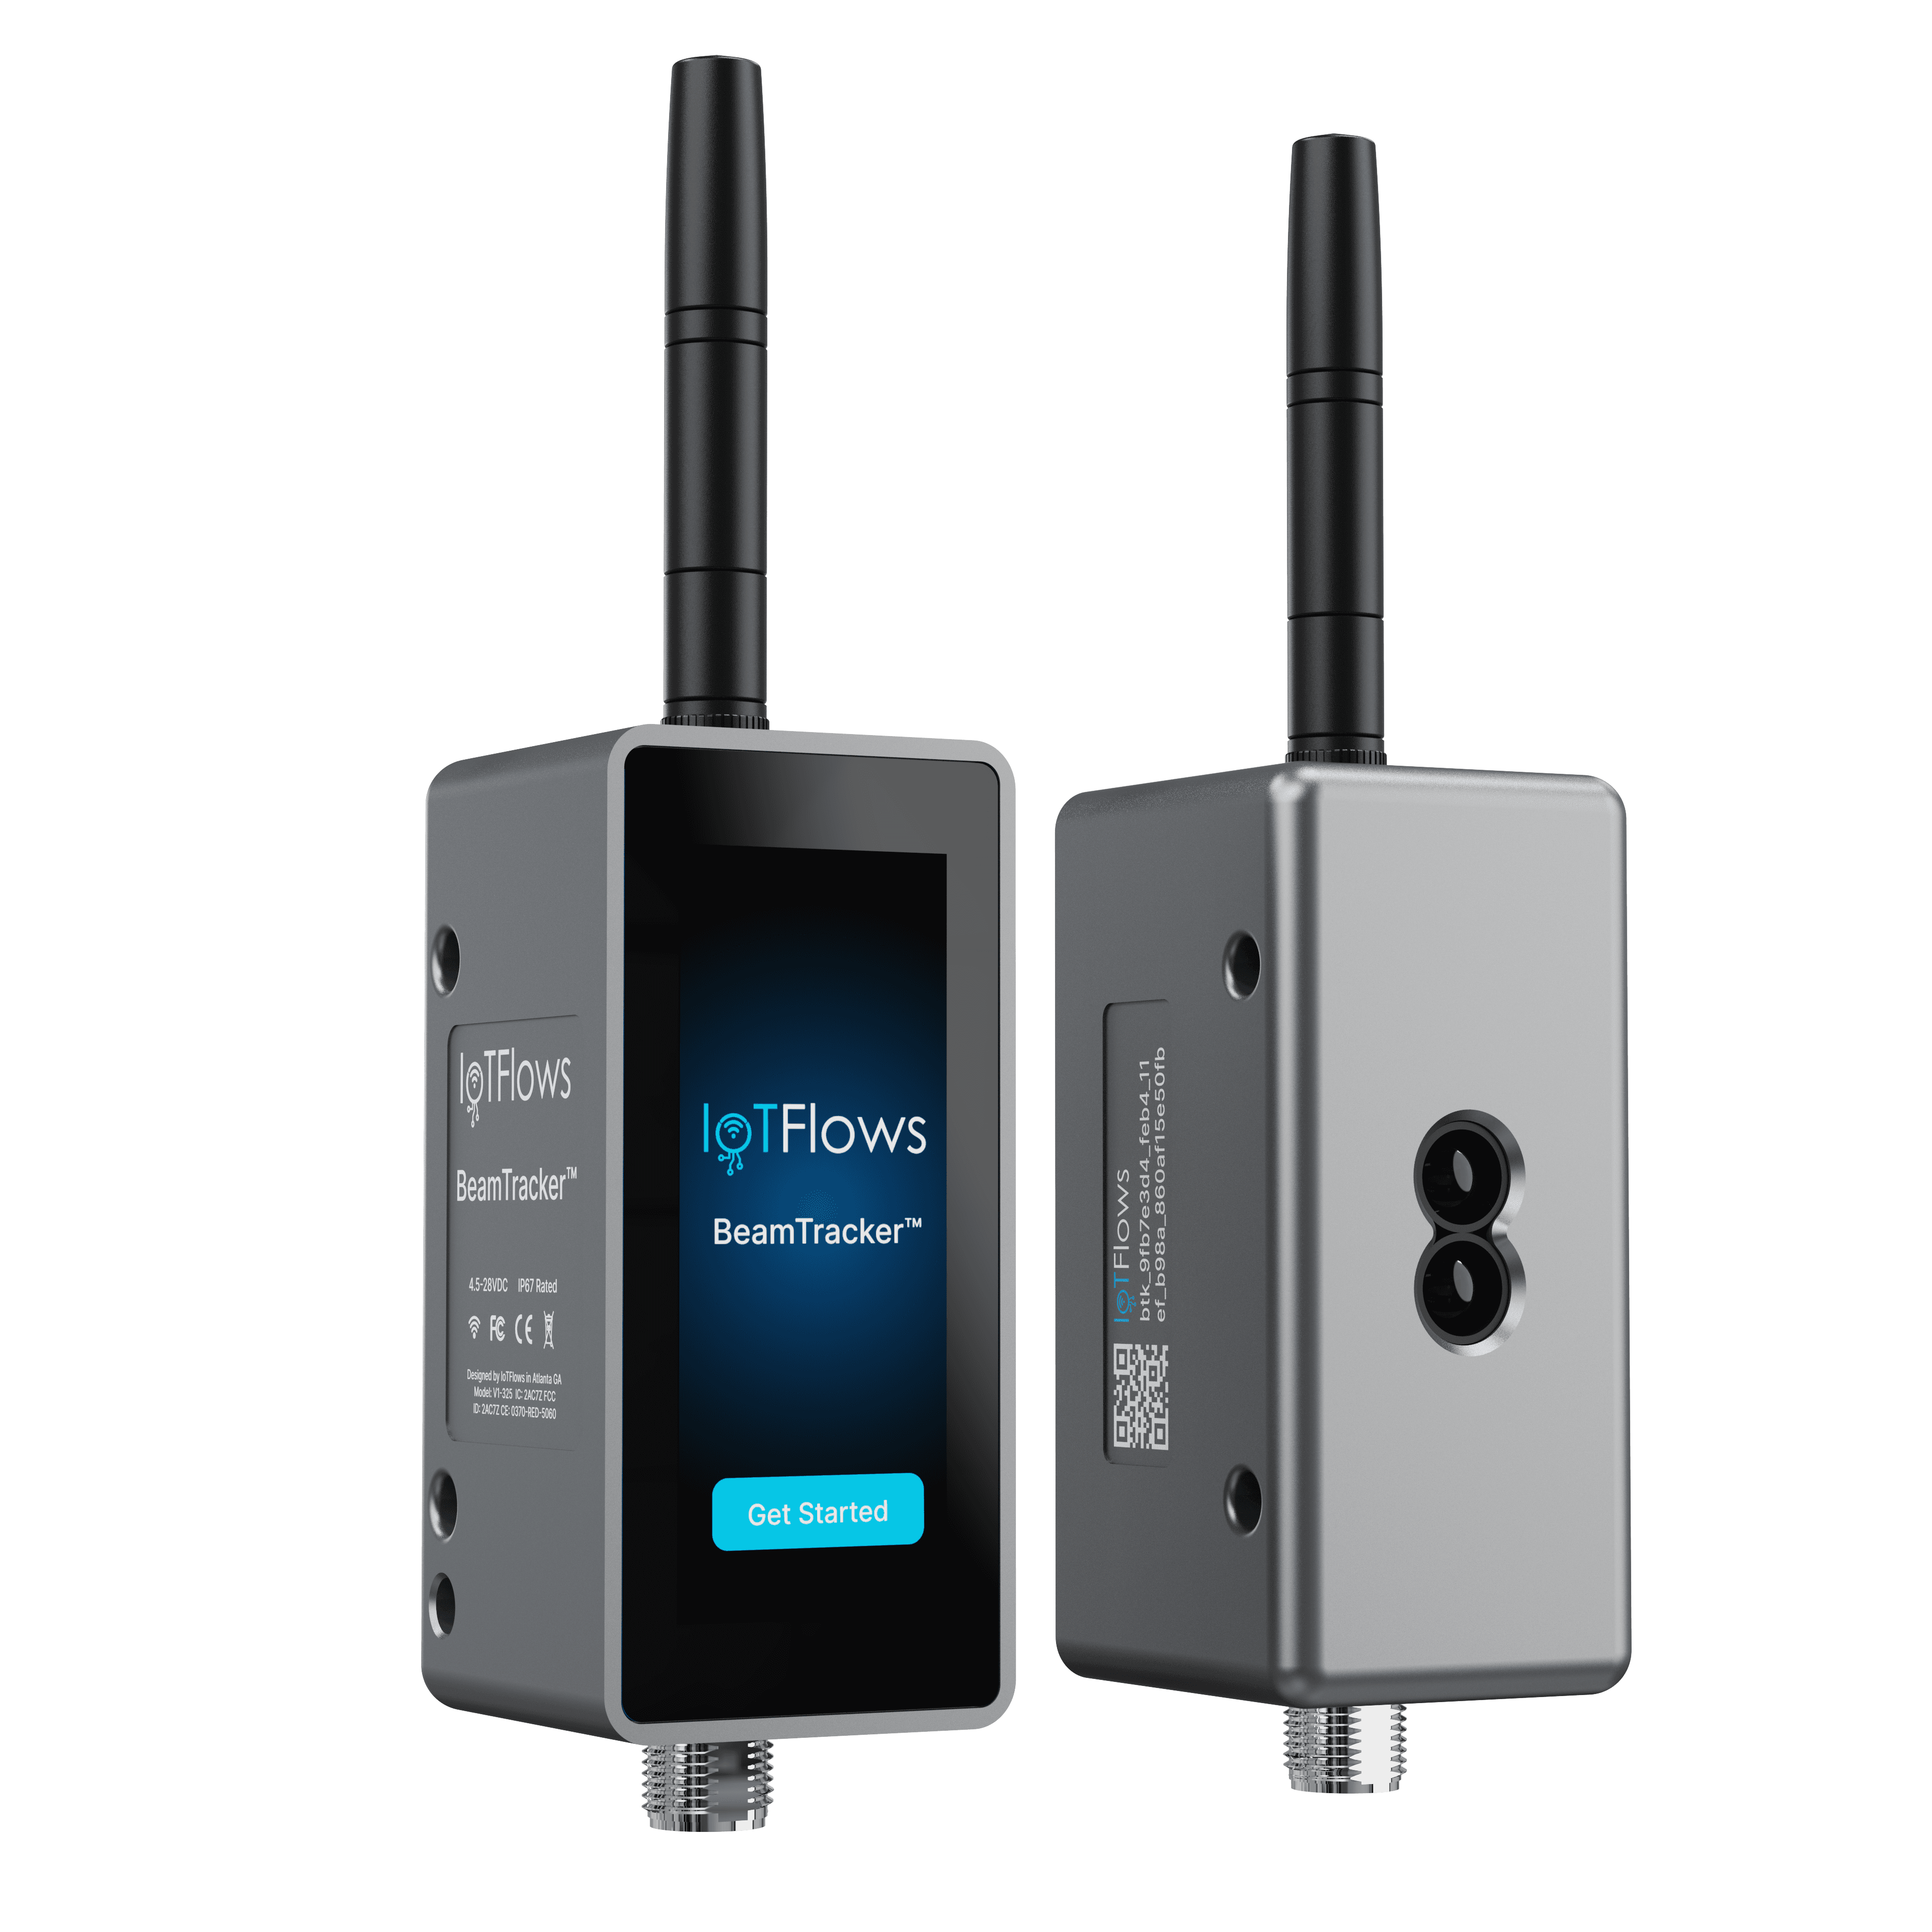
A BeamTracker at every step counts each bottle as it passes, at anything from 20 to 140 a minute, and reads that machine's rate in bottles per minute. See Configure tracking for bottling and packaging lines.
Every line as one cascade
The machines a bottle passes through are grouped into a cascading group, one per line, each with its step number. Step 1 is the reference: every step after it reports its first pass yield, the share of Step 1's bottles that reached it, with the bottles lost and the rate difference against Step 1 underneath. Yield reads green from 95%, amber from 80% and red below that, so a step falling behind stands out on the page.
One changeover for the whole line
When a line switches to a new bottle, one action sets the part on the whole cascade and the operation on each of its machines, so every step keeps counting against the right part from the first bottle of the run. See Cascade a part and operation.
Maintenance by the bottle
In Maintain, each wear part gets a meter that counts the bottles the line has actually made. The Slide Knife's meter counts toward 100,000. The team gets an email as it gets close, and at 100,000 the inspection opens as a work order on its own. Once the knife is inspected, a reset starts the next 100,000. See Trigger maintenance from meter readings.
The line on every screen
The live numbers, first pass yield included, run on TV screens on the shop floor and in the break room, on desktops and on phones, so operators, technicians and managers all see the same line at the same moment. See Display a wallboard on a TV.
Where the bottles go
On a cascade, a line's yield reads step by step. The view below is drawn from a five-step Altium line: Line 2 molded 22,860 bottles between 8 AM and 1 PM and 22,080 of them passed the leak detector: 96.6% first pass yield, 780 bottles lost. The steps in between say where: 148 at the detabber, another 207 by the trimmer infeed, and 351 at the leak detector, the largest single loss on the line. The rate column tells the same story in bottles per minute, so the team can see whether a step is losing bottles or simply running slow.
 A simplified view with sample data: one bottling line as a cascade, with each step's first pass yield, the bottles lost and the rate difference against Step 1.
Because every number is live, a drop shows while the shift is still running. The team talks it through on the floor, helps the operator at that step, and adjusts the line before the losses add up, instead of finding them in a report a week later.
 A simplified view with sample data: all ten bottling lines live on the shop-floor TV, with the Slide Knife's count toward its next inspection along the bottom.
Inspected on the bottle it was due
The same counts drive maintenance. Because the meter counts what the line actually made, the Slide Knife is inspected on the bottle it is due, whether the line ran fast or slow that week. The work order lands in Maintain with the line attached, and nothing depends on someone remembering to check a counter.
 A simplified view with sample data: a production-count meter for the Slide Knife inspection. It climbs to 100,000 bottles about once a day on a line like this one, opens the work order and starts again at each reset.
The Results
From Old Reports to the Live Line
- First pass yield on every step of all ten bottling lines, live, with the bottles lost and the rate difference at each step
- Losses found at the machine that caused them, while the shift is still running, instead of in an end-of-line total days later
- Every bottle counted by BeamTracker at every step, at 20 to 140 bottles a minute
- Maintenance by the bottle: the Slide Knife inspected every 100,000 bottles, with the work order opened automatically
- Production significantly optimized by keeping wear parts on the count they are due and every step on its yield
- Live numbers on the floor, in the break room, on desktops and on phones, in place of reports that took days or weeks
- Issues talked through, operators helped and operations adjusted in real time
- Fewer losses from a missed inspection or replacement, or from an operator unsure of their role in the line
For a plant where every bottle passes through several machines, that is the difference between knowing a line came up short and knowing which step, which hour and how many bottles.
"Now we can talk through issues, help our operators and adjust operations in real time. We used to wait days or weeks for reports, then hold meetings and hope the team knew exactly what had happened. IoTFlows has been a game changer for us."
Steve Petti, Plant Manager, Altium Packaging
The Features Behind It
- BeamTracker at every step of every bottling line for a count of every bottle and each machine's rate. See BeamTracker.
- Cascading groups that read each line step by step. See Group machines into cascades.
- First pass yield, bottles lost and rate difference on every step. See FPY across a cascade.
- Production-count meters that open a work order at the count a part is due. See Trigger maintenance from meter readings.
- Maintain for the work orders, from the first alert to sign-off. See Maintain.
- Wallboards on TV screens across the floor and the break room, with the same numbers on desktops and phones. See Display a wallboard on a TV.