

Injection molding monitoring
Injection molding machine monitoring that counts every shot and every cavity
A sensor on each press counts every shot and multiplies it by the mold’s cavities. Mold-open pauses stay out of your downtime, and every changeover gets a reason.
Trusted by industry leaders
Any press
Every press on the floor, whatever its age
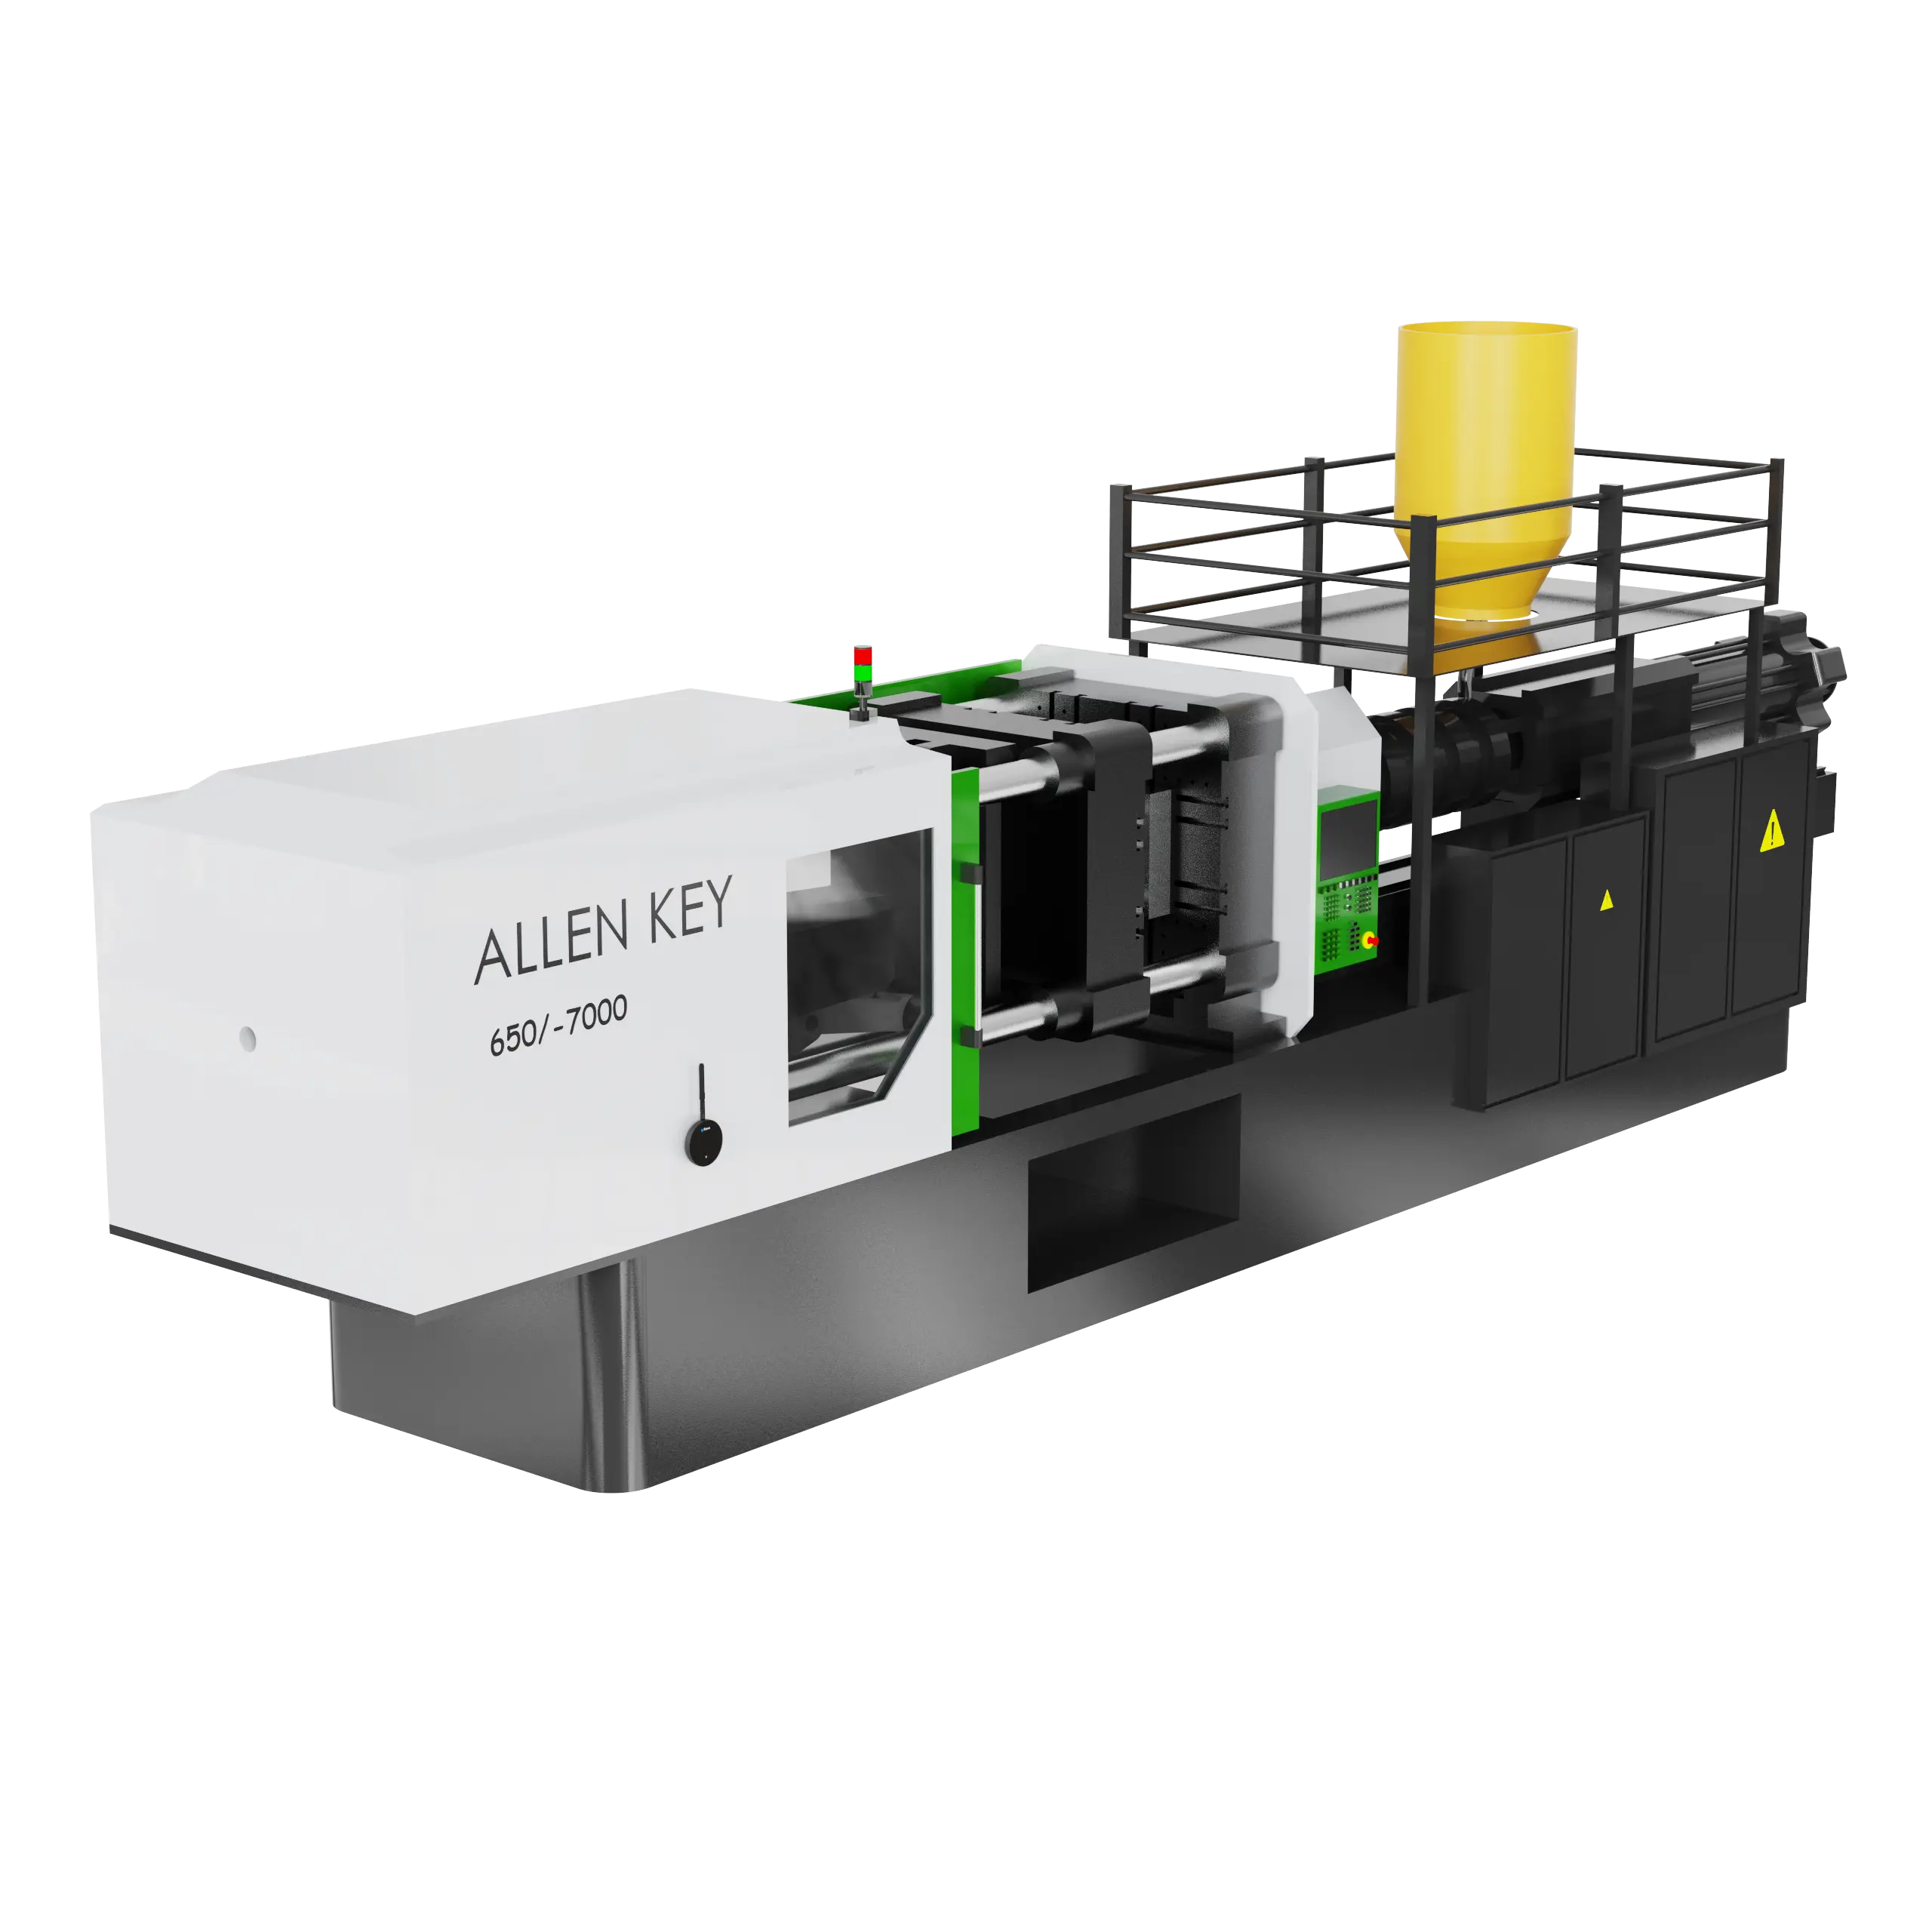
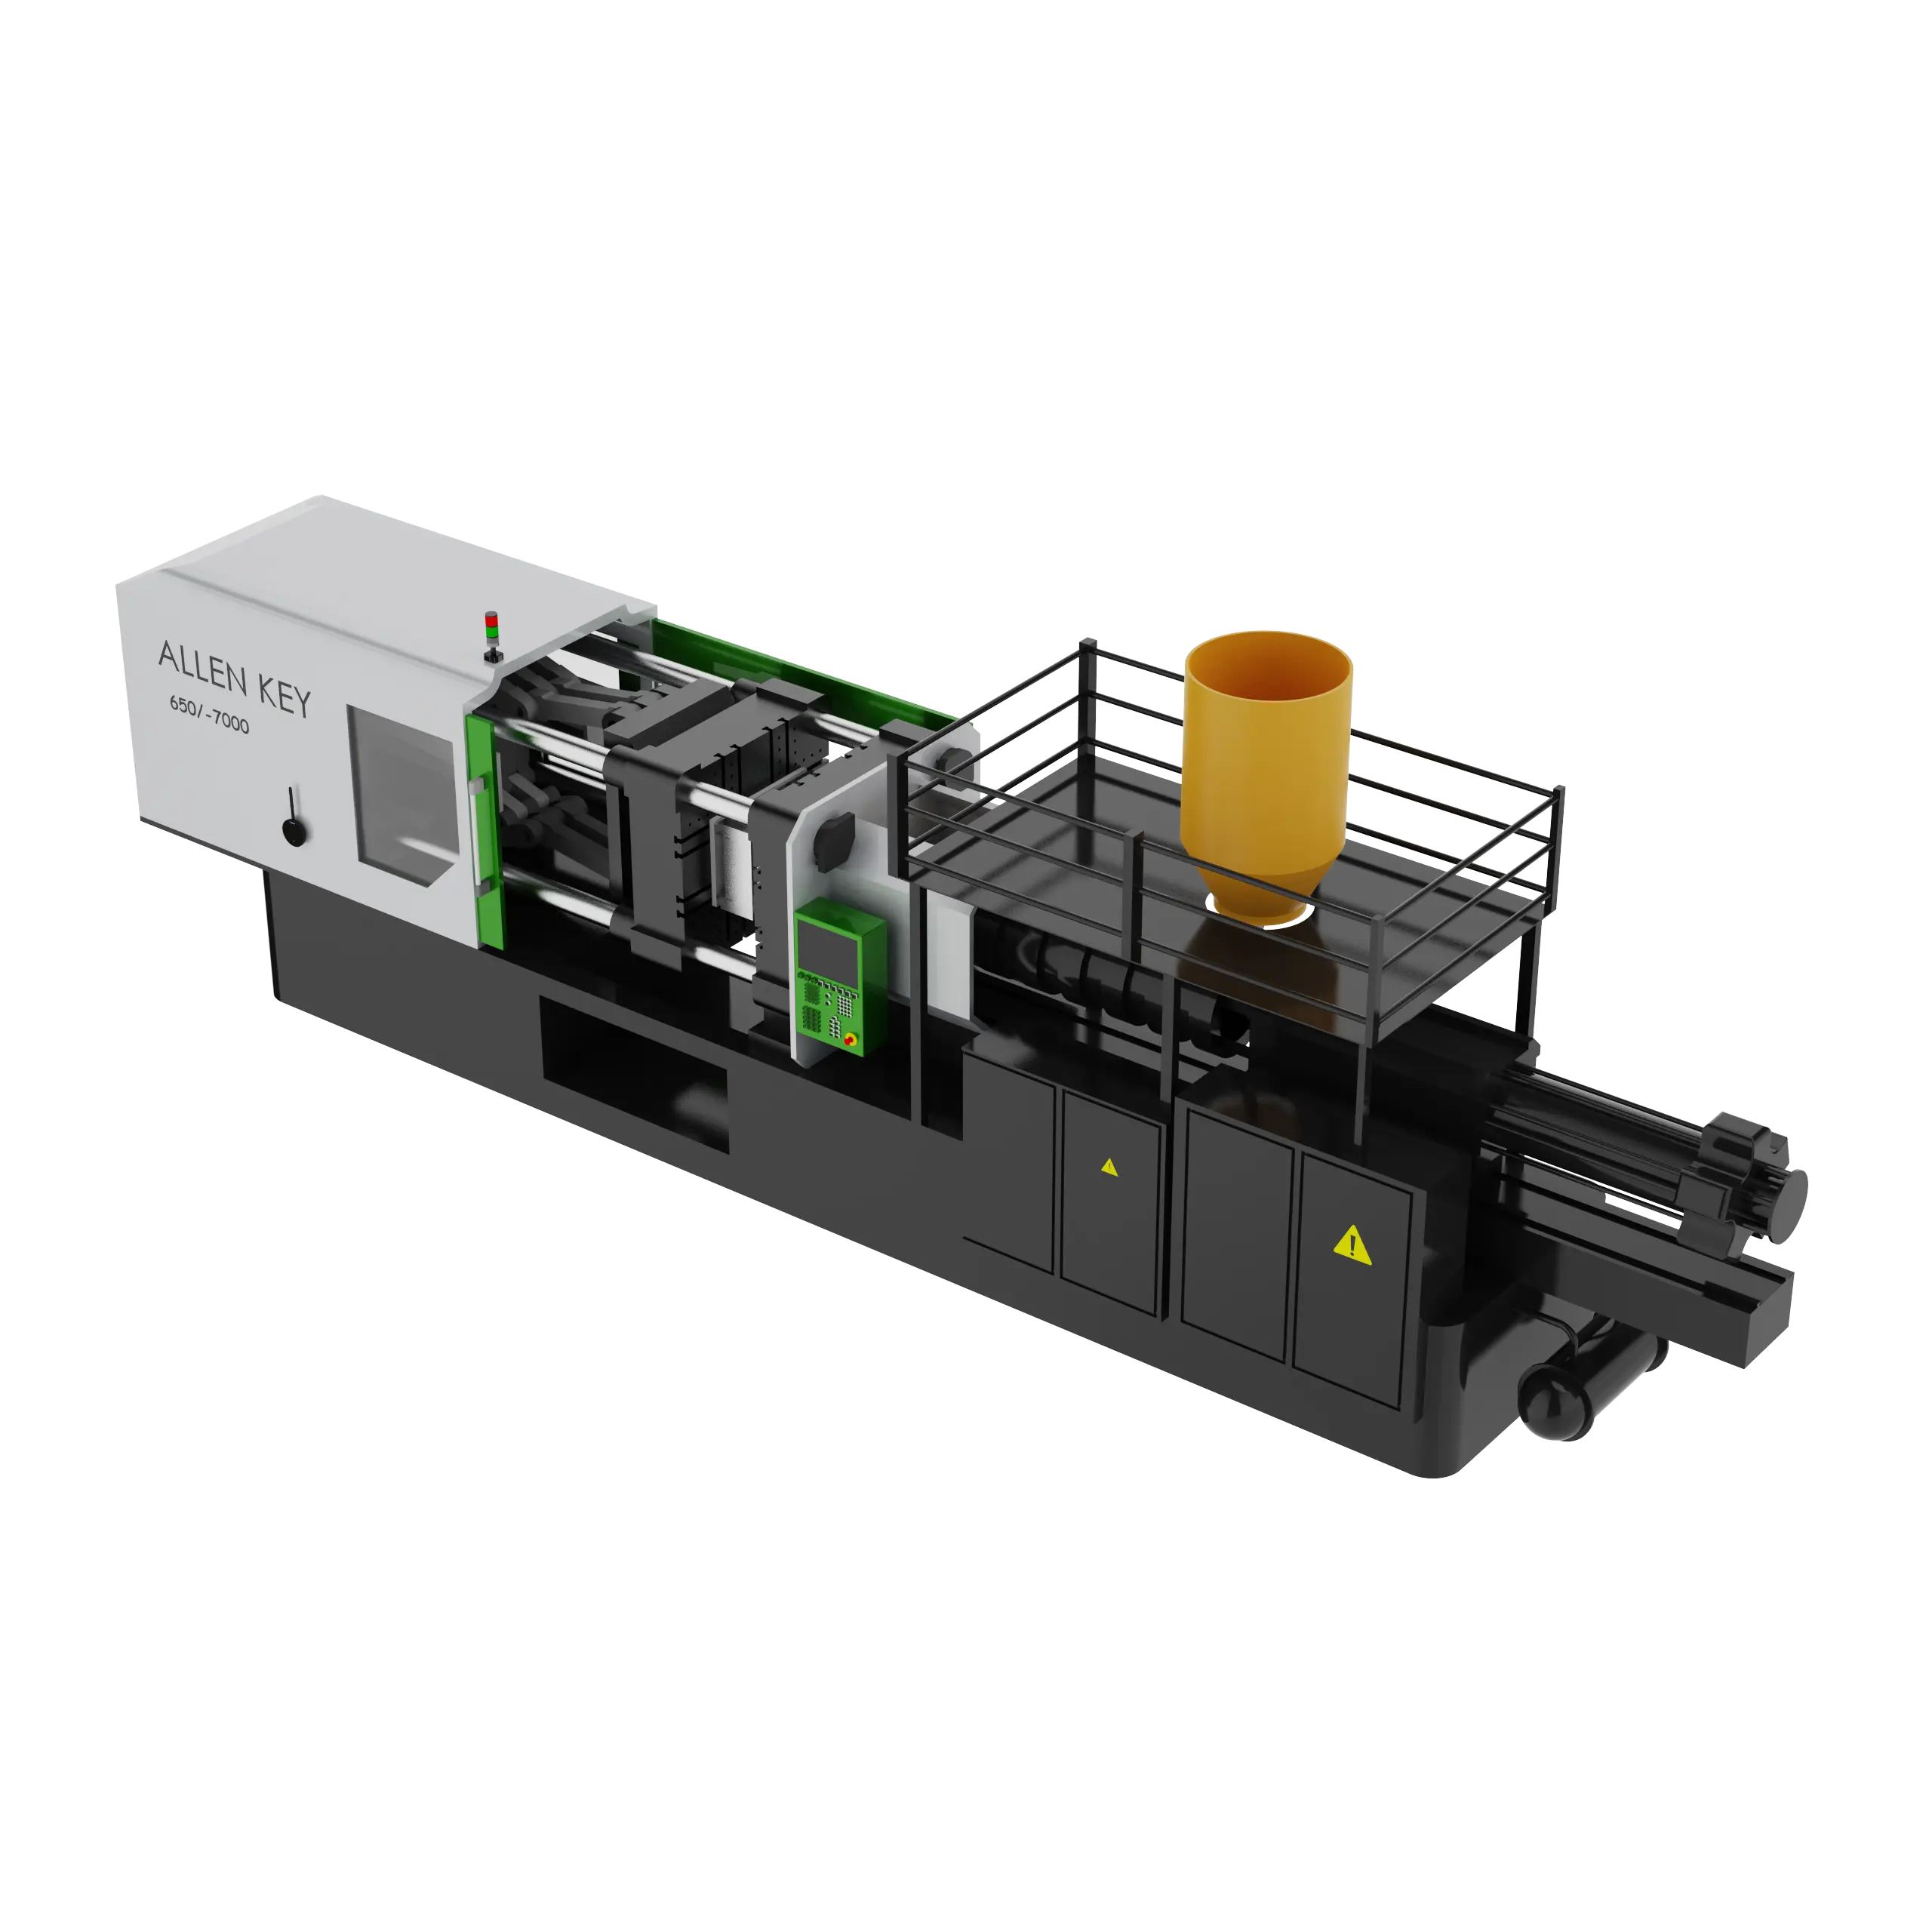
A SenseAi on the injection unit or near the hydraulic pump attaches magnetically in seconds and calibrates in under five minutes. No PLC, no controller connection, no network cable to the press: it connects over 2.4 GHz Wi-Fi or the IoTFlows 4G/LTE router.
A thirty-year-old hydraulic press and last year’s machine report shots, uptime and stops the same way, in one view across every brand.
Shots and cavities
Every shot counted, every cavity multiplied
Continuous Analysis counts the shots from the press’s own steady rhythm. Set the cavity count once per mold and every shot becomes the right number of parts: an 8-cavity mold running 1,300 shots made 10,400 caps.
One operation per mold keeps a 2-cavity and a 4-cavity tool apart, and the count follows the mold through every change.
Short pauses
Mold open is not downtime
Mold open, ejection and mold close break the rhythm for a second or two every shot. The downtime filter turns any pause shorter than a share of the cycle into runtime, up to 200%.
The record keeps only the stops that matter: a material shortage, a mold problem, an operator stopping the press.
Changeovers
Mold and material changes, timed and named
Operators put Mold Change or Material Change on the stop from the press or a phone, and changeovers that always look the same classify themselves with a rule.
The Downtimes report ranks them by the time they cost, so the team knows which changeover to shorten next.
Maintenance by count
Mold maintenance on the count, not the calendar
A Maintain meter counts the press’s output toward a trigger point, such as 200,000 caps on an 8-cavity mold.
Your team gets an email at 85% and the work order opens at 100%, so the mold is serviced when it has earned it.
Scrap
Rejects logged at the press
Operators log short shots, flash or sink marks against the job they are running, with a reason from your own list.
The good count is the one that reaches the report, and every reject is on record by press, mold and cause.
Customer story
Datwyler raised molding efficiency 20% in six months
Datwyler molds precision components on more than 20 injection molding machines in Ontario, California. Every stop carries a reason, and the weekly and monthly reports show which ones to fix next.
- 20%
- higher efficiency across 20+ machines
- 30%
- less material-changeover downtime
- 50%
- less shift-changeover downtime
Challenge
Supervisors could see that machines were down, but not why. With no reasons on the stops, every fix was a guess, and nobody could tell whether it had worked.
Solution
SenseAi on every molding machine, with short stops and the start and end of each shift classified automatically. Operators and supervisors put a reason on the rest, and the team reviews the Downtimes report week over week and month over month.
Products
SenseAi and the Downtimes report.
“By tracking downtime categorization week to week and month to month, we could see exactly where our biggest problems were and track whether our fixes actually worked. The 50% reduction in shift changeover time came directly from acting on patterns we saw in the historical reports.”
See how Datwyler classifies its short stops and shift changes automatically on downtime tracking.
Questions people ask
A SenseAi on each press, on the injection unit or near the hydraulic pump, on 2.4 GHz Wi-Fi or the IoTFlows 4G/LTE router. From it: each press’s live running and stopped state; shots counted with Continuous Analysis and multiplied by the mold’s cavity count; cycle time against the ideal and a goal for every shift; a downtime filter that keeps mold-open pauses out of the downtime record; Mold Change and Material Change reasons, with rules that classify routine changeovers; scrap logged with a reason; Maintain meters that open mold maintenance on a part count; and the same numbers on a TV, a tablet and a phone.
Yes. Set QTY/OP on the operation to the mold’s cavity count and every shot counts as that many parts: a four-cavity mold running 100 shots made 400 parts. Create one operation per mold, so a two-cavity and a four-cavity tool for the same part stay separate.
Yes. The sensor reads the press’s vibration from the outside through a magnetic base, so a hydraulic press from the 1990s and a new machine report shots, uptime and stops the same way, across every brand, with no PLC, no controller connection and no network cable to the press.
No. Each sensor connects over 2.4 GHz Wi-Fi, or through the IoTFlows 4G/LTE router where there is no Wi-Fi or you want the devices off the plant network. Devices only connect out, over HTTPS on port 443.
With the downtime filter on the operation: any stop shorter than a set share of the cycle time counts as runtime. It takes 0 to 200%, and 200% is the usual starting point for a molder. On a 22-second cycle every pause under 44 seconds stays runtime, while material shortages, mold problems and operator stops stay in the downtime record.
Yes. Each operation carries an ideal cycle time, and the shift goal and the pace come from it. Every stop longer than the filter lands on the downtime record with its start, end and duration, and operators or automatic rules put a reason on it.
60 to 75% when an operator loads inserts or takes parts off, 75 to 85% fully automatic, and 85 to 90% lights-out around the clock. Set each press’s goal from its own baseline plus 5 to 10%, and log rejects so the good count is the one you compare.
Yes, with Maintain. A meter counts the press’s parts toward a trigger point, for example 200,000 caps on an eight-cavity mold. It can email at 85%, email at the trigger and open a work order at 100%, and a reset after the service starts the next cycle. Maintain starts at $500 per month.
SenseAi is $149 per press, bought once. The Pro plan is $119 per device per month billed monthly, less on annual and three-year contracts and from 10 devices, and 50 or more devices are quoted. Maintain starts at $500 per month. A pilot puts IoTFlows on 10 to 25 machines for four weeks with no commitment to buy.
Documentation
Want the detail? These guides walk through each feature step by step.
- Configure tracking for injection moldingContinuous Analysis, one operation per mold, cavities as QTY/OP.
- Set cycle times and downtime filtersThe ideal cycle and the filter that keeps mold-open pauses out.
- Count runtime or parts with metersMold maintenance on a part count, with a work order at 100%.
- Log scrap and manage scrap reasonsShort shots, flash and sink marks, logged at the press.
Count your first press this week
Start with 10 to 25 machines for four weeks, with no commitment to buy. A SenseAi goes on the presses you already run.